01 / 07
A tower is a stack of cans
Each section is a string of rolled cans, welded end to end. The flanges at each end decide whether the tower stands straight.
Scroll to see how it is built · drag to turn it round
You are using Internet Explorer and will not be able to use our website properly.
Please change to an up-to-date browser for ideal presentation of the website.
Tower sections rolled from heavy plate, welded seam to seam, and finished with machined L-flanges so each section bolts square onto the next.
Scroll: the camera moves to each part in turn and ends on the exploded view. Drag to turn it round yourself.
01 / 07
Each section is a string of rolled cans, welded end to end. The flanges at each end decide whether the tower stands straight.
Scroll to see how it is built · drag to turn it round
02 / 07
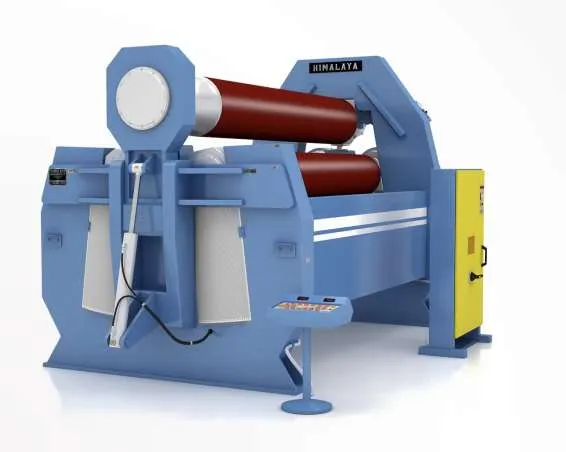
Plate is cut and bevelled, then rolled to diameter on the plate rolls and seam welded. The cans are fitted up on rollers so their seams stagger, as the design asks.
03 / 07
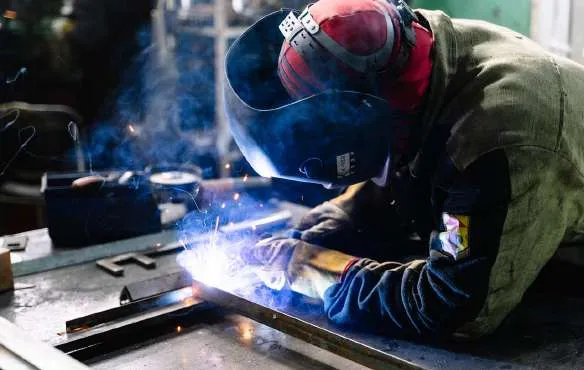
Longitudinal and circumferential seams run on the submerged-arc line, then are inspected to the client plan.
04 / 07
The L-flange is welded to the end can in a sequence that keeps its face flat, so the joint closes without gaps when the bolts are tensioned.
05 / 07
Around a hundred bolts on the inner circle join two sections. We supply the joint ready to bolt, with the holes drilled to match the next section.
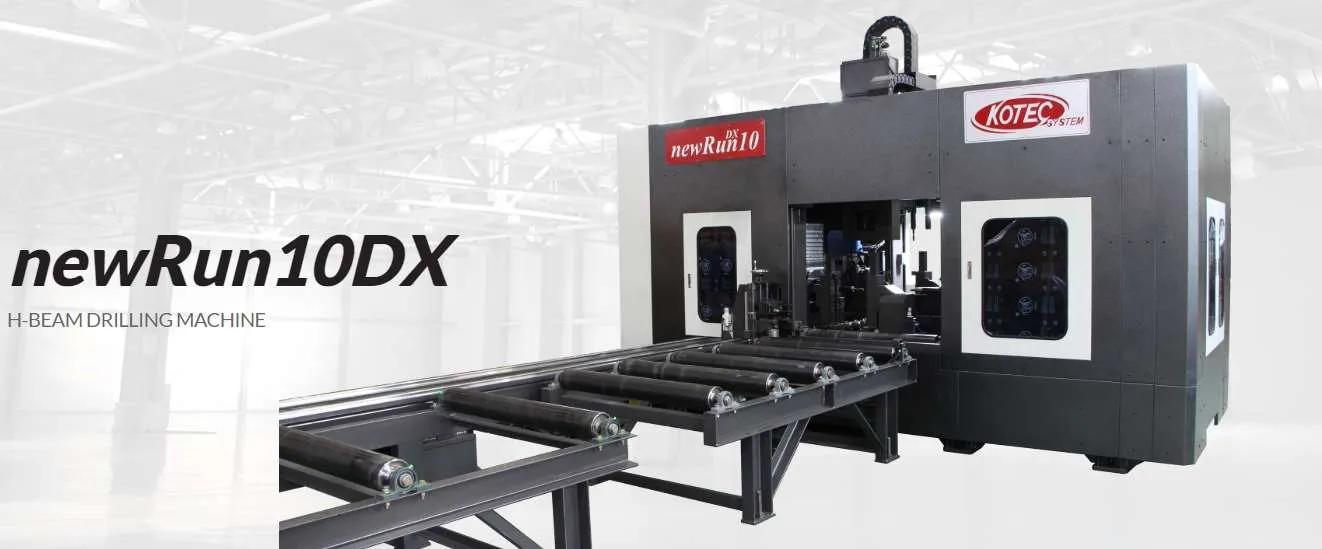
Used here for: The bolted joint
Heavy profiles that need precise holes, where plasma cannot do the job: the lower structure and panel borders of a ground flare, and every bolted PEB and multi-storey frame.
06 / 07
The heavy door frame is rolled to the shell radius and welded in; platforms and ladders go in before the section leaves.
Used here for: Door and internals
In 2024 we were the only buyer of Deratech’s 20 kW, 12 m laser.
07 / 07
Cans, seams, flanges, bolts, door frame and internals.
We fabricate to your drawings and prove the fit in our own bay before anything ships. Open any line for the detail.
Talk to an engineer Inverter & Transformer Skids
Renewables · Wind
 Nacelle & Hub Assembly Fixtures
Renewables · Wind
 Monopile & Transition Piece Steel
Renewables · Wind
 Offshore Tripod Foundations
Renewables · Wind
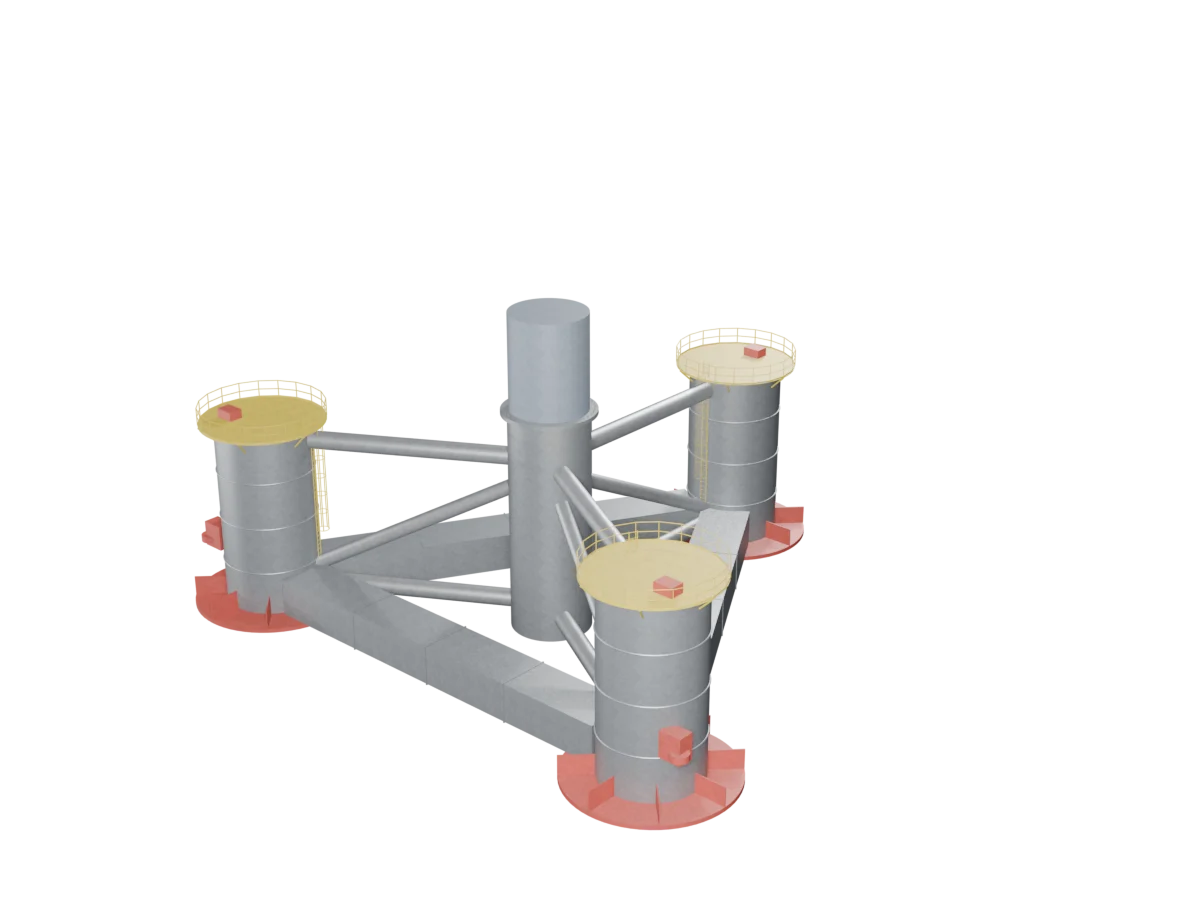 Floating Wind Foundation Blocks
Renewables · Solar
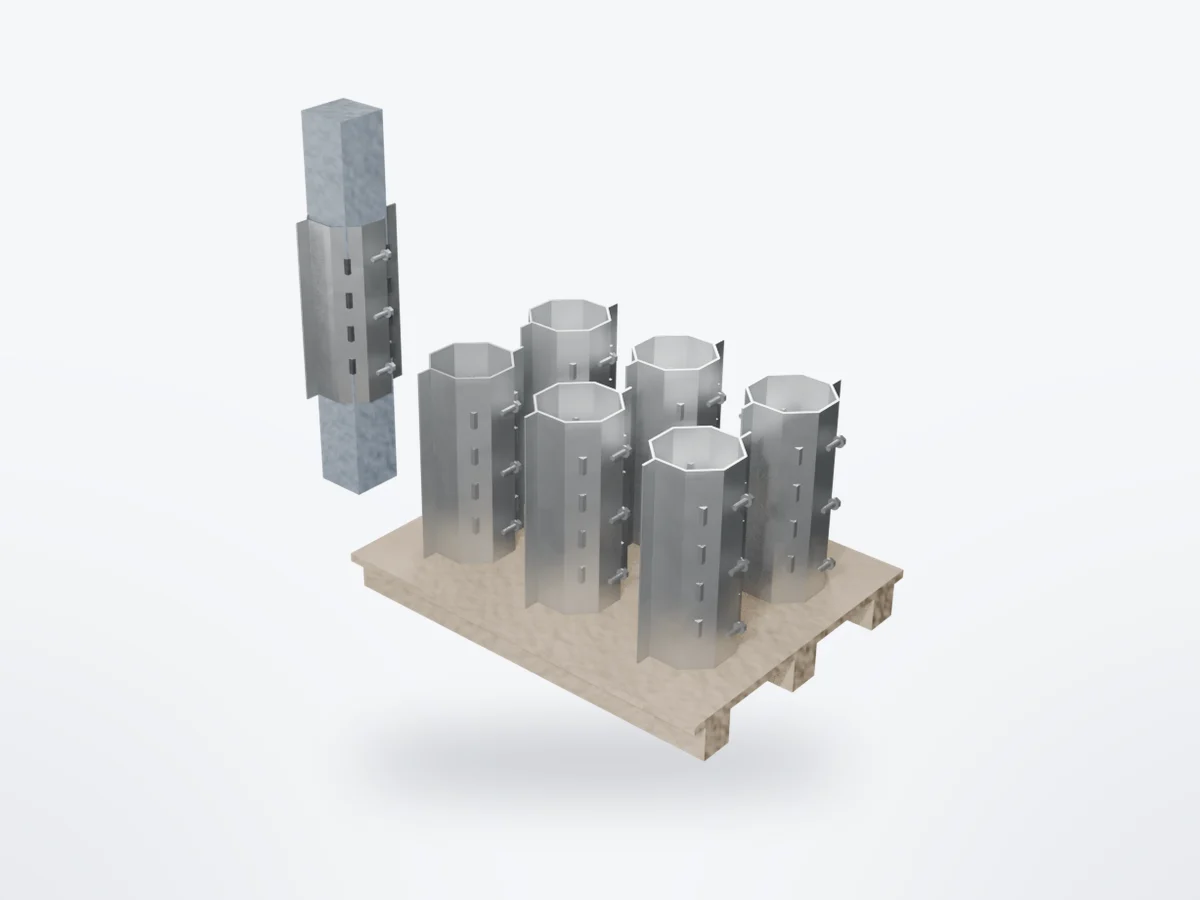 Tube Connector Preassembly for Solar Trackers
Renewables · Solar
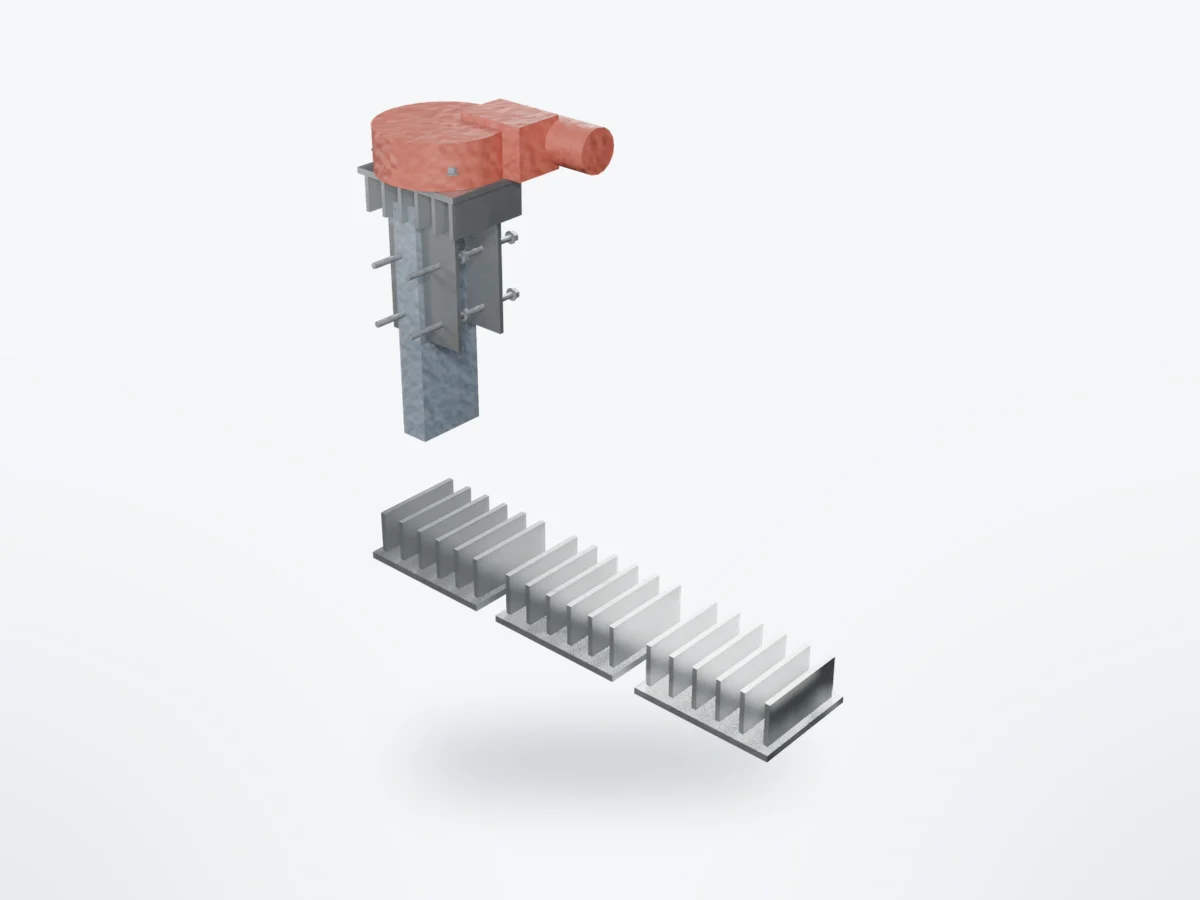 Slew Drive Seats for Solar Trackers
Renewables · Solar
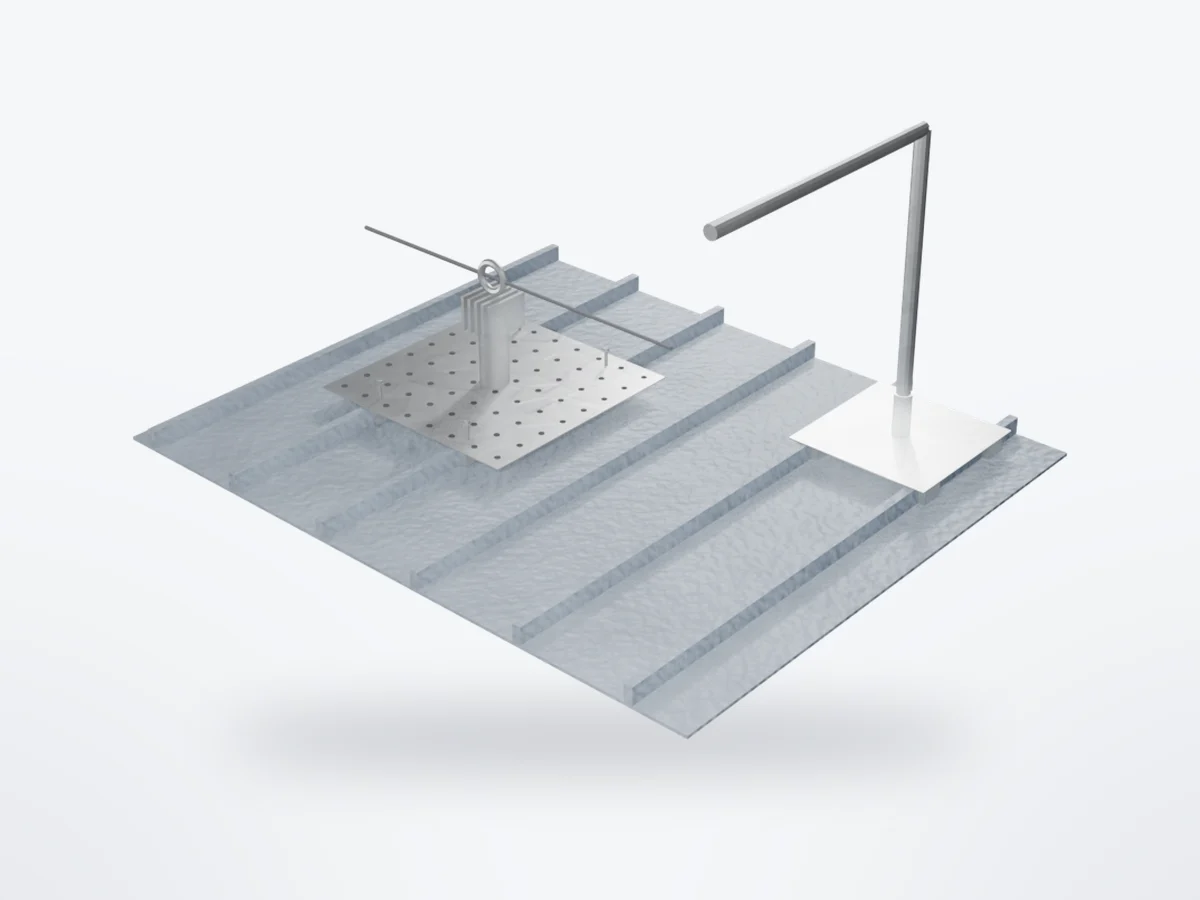 Base Plates for Lifeline & Handrail Mounting on Solar Rooftops
Renewables · Solar
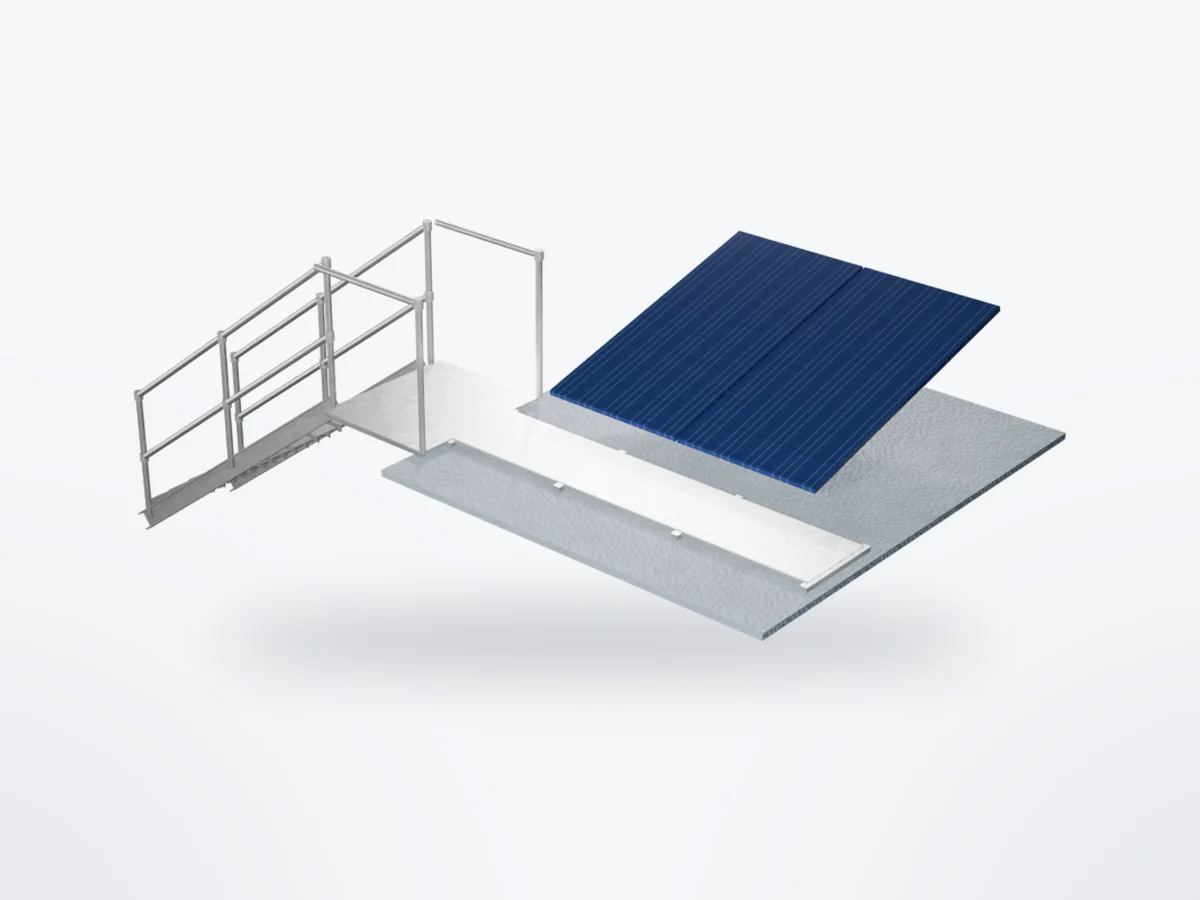 Solar Walkways & Stairs
Renewables · Wind
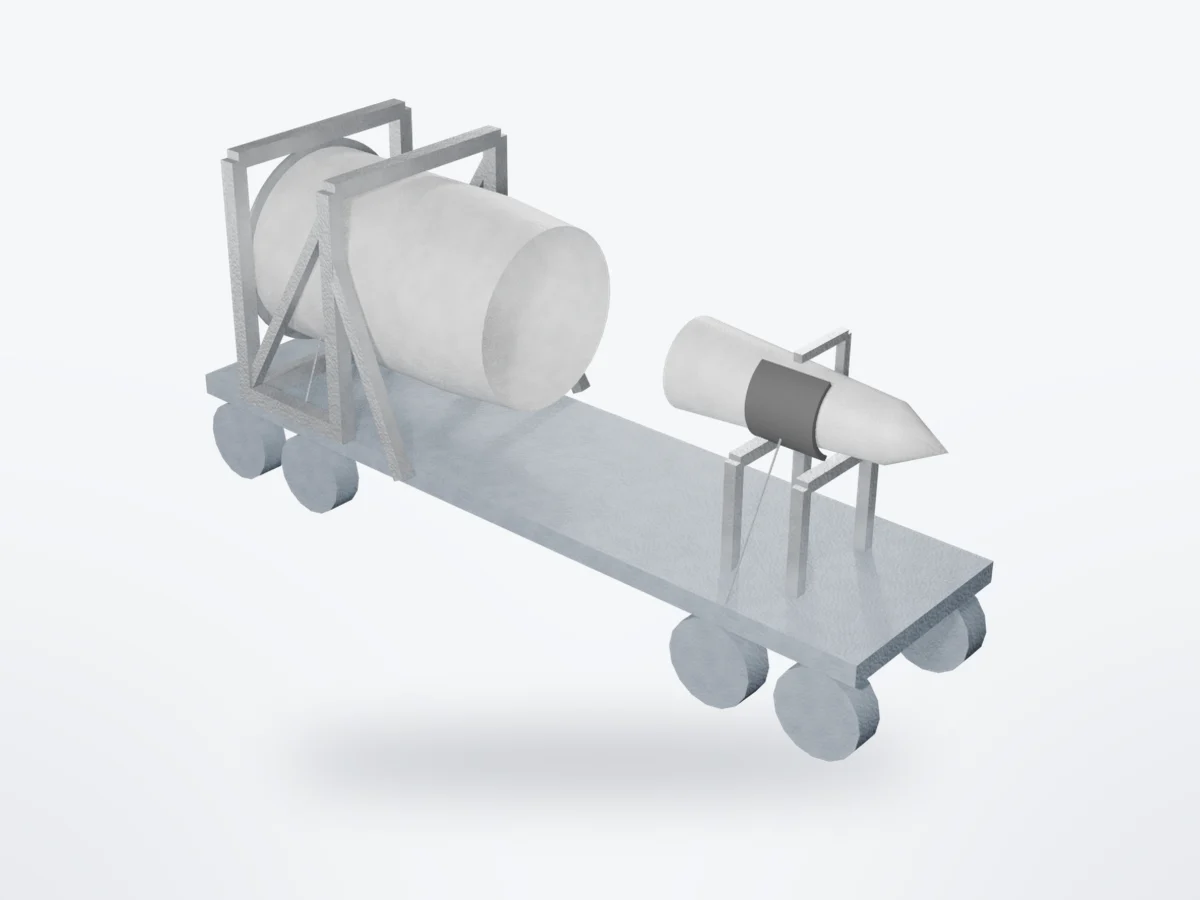 Blade Transport Fixtures
Renewables · Wind
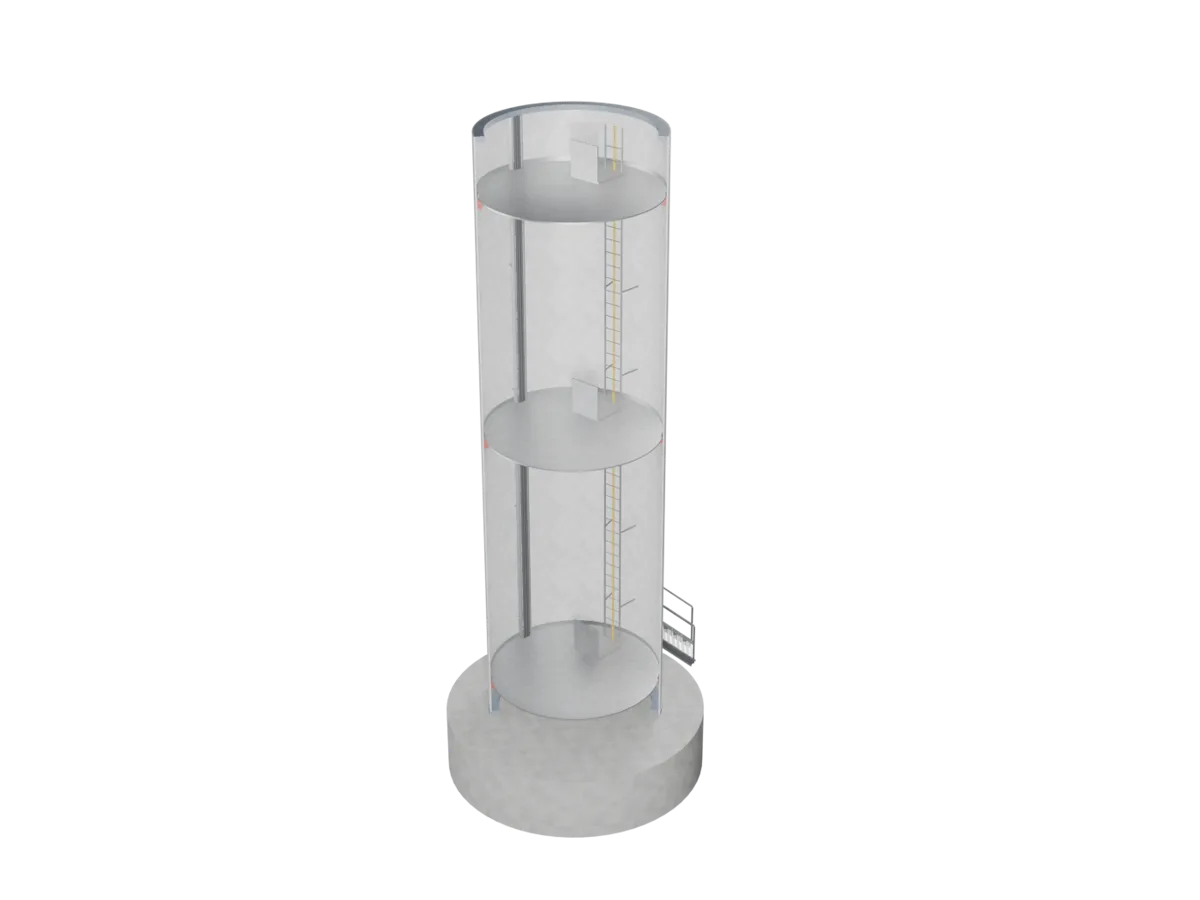 Wind Tower Internals
Renewables · Wind
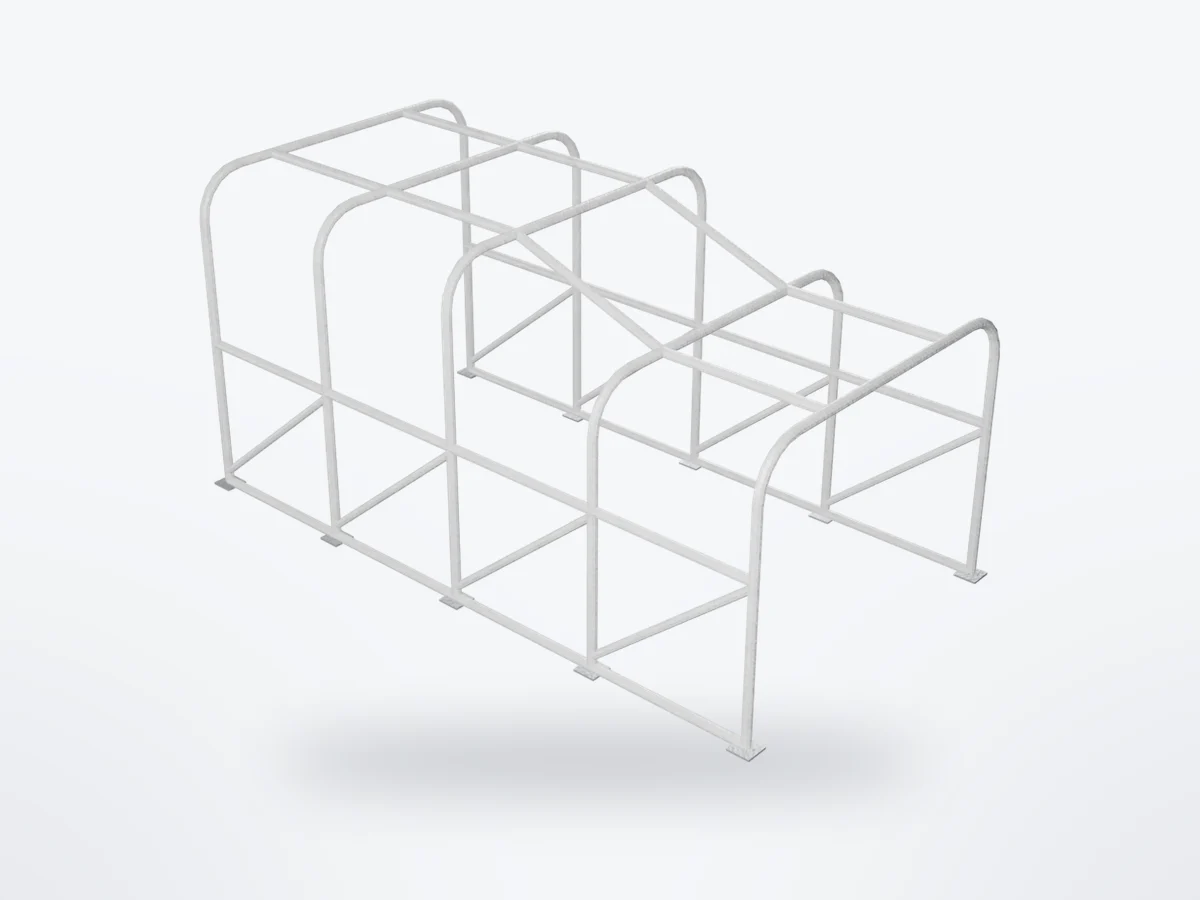 Nacelle Skeleton Frames
We fabricate to your design, from plate to a packed container. An engineer will tell you honestly how we would build it.